For manufacturers managing high-value raw materials, knowing how much inventory is available is only part of the picture. Teams also need to know where that material is physically located and whether its system record reflects what is actually happening on the plant floor.
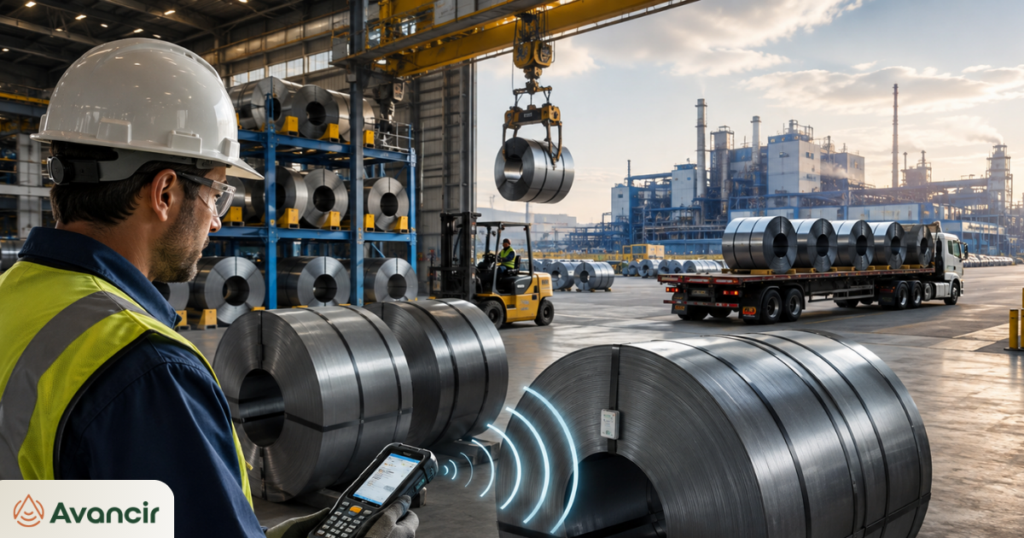
A leading U.S. steel manufacturer faced that challenge while managing steel coils across multiple facilities. Coils could be stored in defined rack locations or general storage areas and moved as production and fulfillment needs changed. When those movements were not reflected accurately in the system, employees could spend additional time locating material, confirming availability, and reconciling physical inventory with digital records.
Avancir implemented an RFID-based material tracking solution designed around the manufacturer’s existing storage and movement processes. The system gives employees a more accurate view of coil locations while using workflow logic to connect material movement with the appropriate business status.
The Challenge: Locating High-Value Material Across Multiple Facilities
Steel coils represent significant inventory value, and their locations can affect decisions well beyond the storage area.
When a coil could not be found where the system indicated it should be, employees had to determine its actual location before the next production or fulfillment step could continue. At scale, those discrepancies could influence production planning, procurement decisions, fulfillment speed, and how effectively the manufacturer used material already on hand.
The manufacturer needed a tracking process that could account for coils across three plants while accommodating different types of storage. A coil placed in a designated rack needed to be associated with that rack, while material in a general storage area still needed enough location context for employees to find it quickly.
Simply identifying an RFID tag would not solve that problem. The system also had to understand where the coil was, how it had moved, and what that movement meant operationally.
The Solution: Mobile RFID With Location-Aware Workflows
Avancir designed the deployment around mobile RFID data capture rather than requiring fixed RFID infrastructure throughout each facility.
Employees use mobile computers to identify material and support tracking workflows as coils move through the operation. Location logic within the system accounts for both defined rack positions and general storage areas, allowing movements to be associated with the appropriate physical location.
This approach gives the manufacturer flexibility to track material across different storage environments without treating every area of the plant the same way.
Behind those mobile workflows, the Avancir Monitoring Engine applies configurable business rules to RFID and operational data. The platform can support location updates, automated coil status transitions, material movement workflows, traceability, exception handling, and plant-specific logic.
The distinction matters because collecting an RFID read is only one part of material tracking. The system also needs to determine which coil moved, where it moved, and how that event should affect the information employees rely on.
Instead of requiring users to manually reconcile every physical movement with a separate system transaction, Avancir helps connect activity on the plant floor with the digital record of the material.
Connecting Plant-Floor Activity With Microsoft Dynamics 365
The next phase of the deployment is planned to connect Avancir directly with the manufacturer’s Microsoft Dynamics 365 ERP environment.
That integration is intended to allow coil activity and location information to move between plant operations and the enterprise system, giving teams a more timely view of where material is and what is happening to it.
Keeping those systems aligned is especially valuable in a multi-site operation. Procurement, production, and fulfillment decisions depend on inventory information that reflects physical reality, not just the last manually recorded transaction.
The Results: Better Visibility Into Coil Location and Status
The RFID solution now provides real-time visibility into tagged steel coils across designated storage locations and facilities.
Employees can locate high-value material faster and trace coil movement with less reliance on manual inventory reconciliation. More accurate location information also helps reduce the risk of material being treated as missing, delayed, or unavailable when it is physically present elsewhere in the operation.
The system supports several operational improvements, including:
- Faster access to coil location information
- Improved material traceability
- Fewer misplaced, delayed, or unnecessarily scrapped materials
- Better inventory information for procurement decisions
- Faster fulfillment workflows
- Improved utilization of existing material
- Less manual inventory reconciliation
The architecture is also designed to extend beyond the current deployment, with additional facilities being evaluated or planned for future rollout.
Why Material Tracking Requires More Than RFID Reads
The value of this deployment comes from connecting RFID data with the way the manufacturer actually stores and moves material.
A tag read can identify a coil, but it does not automatically explain whether that coil was placed in a rack, moved into general storage, advanced to another operational step, or encountered an exception. Those decisions depend on workflow and location logic.
Avancir provides that layer between RFID data and the manufacturer’s operational systems. By applying business rules to material movements, the platform turns individual data-capture events into information that employees can use to locate inventory, maintain traceability, and make production and fulfillment decisions.
For manufacturers managing valuable raw materials across multiple plants, that connection helps move inventory tracking away from periodic reconciliation and toward a more current representation of what is actually happening on the floor.
Learn more about how Avancir supports RFID inventory management across manufacturing operations.